

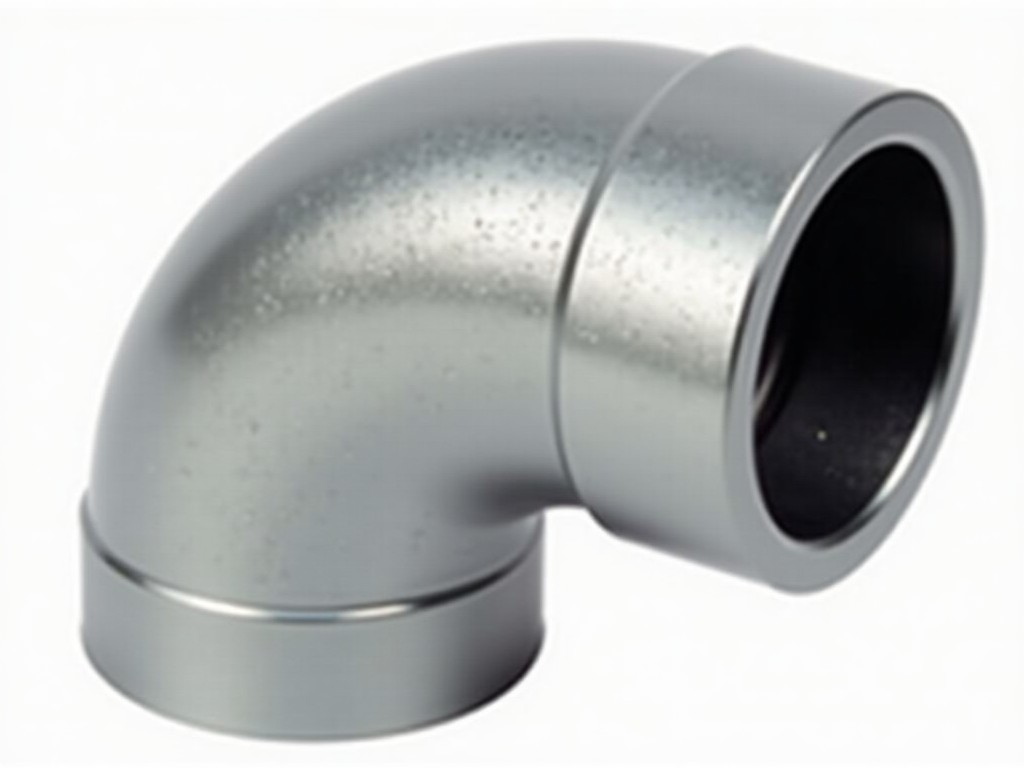
Purpose‑built long‑sweep 3‑inch 90° elbow with 36‑inch centerline radius (R/D≈12) for piggable, low‑turbulence and high‑pressure pipelines. Verified ASME B16.49 compliance, traceable material certificates, and export‑ready packing.
🇺🇸 USA · 🇪🇺 Europe · 🌍 Export Grade
Purpose‑built long‑sweep 3‑inch 90° elbow with 36‑inch centerline radius (R/D≈12) for piggable, low‑turbulence and high‑pressure pipelines. Verified ASME B16.49 compliance, traceable material certificates, and export‑ready packing.
🔒 Your inquiry is protected under our privacy policy. Reply within 8 business hours.
In our 15+ years of exporting pipe fittings, we repeatedly hear the same frustrations from pipeline contractors and plant operators:
💰 Hidden long‑radius pricing premiums — Many suppliers quote an automatic 60–100% price uplift for R/D ratios above 3, without added value. You end up paying for “custom work” that is actually a standard induction‑bending process.
📉 Quality failures in the bend zone — On poorly manufactured long‑radius elbows, wall thinning in excess of 15% and ovality beyond 5% are common. These are direct causes of burst and fatigue failures in service.
🚢 Over‑priced ocean freight — Due to the long swept profile, a 36‑inch radius 3‑in elbow occupies large crate volume. Inexperienced forwarders charge you dimensional weight instead of actual weight, inflating logistics cost by up to 40%.
📄 Missing material traceability — Without EN 10204 3.2 certificates, full chemical analysis, and hardness test reports, your QA/QC team will reject the batch on arrival. Rework and project delay then follow.
We designed our entire production and export workflow to eliminate these four pain points. Get a transparent landed‑cost quote now.
This 3 in 90 degree 36 in radius elbow is a factory‑made, wrought‑steel induction bend designed for pipeline systems that require minimal pressure drop, safe pigging, and reduced erosion at direction changes. The 36‑inch centerline radius (equivalent to R/D ≈ 10.3 based on OD, or 12D based on nominal bore) places it far outside the standard 1.5D long‑radius range, making it an engineered solution for demanding flow assurance applications.
| Parameter | Value |
|---|---|
| Nominal Pipe Size | 3 in (DN80) |
| Bend Angle | 90° (±0.5°) |
| Centerline Radius | 36 in (914.4 mm) |
| R/D Ratio (OD based) | 10.3 |
| Outside Diameter | 3.5 in (88.9 mm) |
| Wall Thickness Options | Sch 10S / 40 / 80 / 160 |
| Center‑to‑End (C) | 36 in (914.4 mm) both ends |
| Tangent Lengths | 12 in (305 mm) standard, custom available |
| Arc Length (90°) | 56.55 in (1436.3 mm) |
| Manufacturing Std | ASME B16.49 / ASME B16.9 |
| End Preparation | Butt‑weld (BE) / Flanged / Grooved |
EN 10204 3.1 / 3.2 material certificate
Chemical composition & mechanical properties report
Dimensional inspection report (with photos)
Hydrostatic test certificate (on request)
Heat treatment chart & hardness test results
NDT reports: PT / UT / RT as specified
Wooden stillage / steel frame crate
Dimensional weight optimization saves 15–35% freight
Multiple elbows stacked with corrugated spacers
FOB/CIF/DDP terms — we handle customs
Engineering Note: For a 90° bend, the center‑to‑end dimension equals the centerline radius. Therefore both ends of this elbow are 36 in from the true center of the arc. This long tangent‑free profile reduces flow turbulence and pig impact loads. Need a different wall schedule or a custom tangent? Our in‑house engineering team can confirm within 24 hours.
A standard 1.5D elbow has a loss coefficient (K) of approximately 0.9–1.2 for turbulent flow. By increasing the radius to 36 inches, the directional change is distributed over an arc length of 56.55 in, reducing the K value to roughly 0.15–0.25. In a pipeline with 50 bends, this translates to a measurable reduction of 0.5–2.5 bar in total frictional loss — reducing pump energy consumption by 6–11% in long‑distance transfer systems.
Intelligent pigs (smart pigs) used for ILI typically require an R/D ratio of at least 3D. With an R/D ratio of ≈10–12D, this elbow easily clears both conventional foam pigs and high‑resolution MFL/UT inspection tools. Operators reduce the risk of stuck pigs and can maintain regulatory compliance with PHMSA / API 1160 integrity management programs.
In slurry, pneumatic conveying, and sand‑prone multiphase flow, elbow erosion is directly proportional to the impact angle and particle velocity. A gradual sweep means particles skim along the outer wall with reduced impingement angle. Independent test data from the University of Tulsa Erosion/Corrosion Research Center shows that increasing bend radius from 1.5D to 10D decreases erosion rate by up to 65% at 10 m/s gas velocity with 500‑micron sand.
📄 Structural Integrity Reference: Published finite‑element research on pipe bends confirms that curved geometry creates cross‑sectional ovalization under external load, accounting for the greater flexibility of elbows (Conference paper, “Elbow Stress Indices Using Finite Element Analysis”). In an R6 failure assessment diagram (FAD) context, dedicated defect‑assessment guidance for elbows is underpinned by the reference‑stress J scheme (“Reference Stress Method for Defective Elbows – R6 FAD Assessment”). These published methods allow our engineering team to verify that a 36‑in radius design keeps stress‑intensification factors well within ASME B31.3 allowable limits.
Material selection is the most critical decision for a special‑radius elbow. We manufacture the 3‑in 36‑in radius elbow in the following grades, each traceable to mill origin:
ASTM A234 WPB — most common, good weldability
ASTM A420 WPL6 — low‑temperature service down to −50°F
ASTM A234 WP11 / WP22 — high‑temp and creep‑resistant
ASTM A403 WP304/304L — general corrosion resistance
ASTM A403 WP316/316L — marine & chemical service
Duplex (S31803/S32205) — high‑strength, chloride stress‑corrosion resistance
✅ Compliance Highlights: Our elbows are manufactured to ASME B16.49 (factory‑made induction bends) and optionally verified to ASME B16.9 for butt‑welding fittings. All welding (if any) follows ASME Section IX procedure qualifications. Where applicable, we provide CE (PED 2014/68/EU), RoHS, ISO 9001:2015, and API Q1 documentation to satisfy US and EU procurement requirements.
Because the radius is 10× the pipe OD, cold bending or a standard push bender is not viable. We manufacture these elbows using high‑frequency induction bending (also called: hot induction bending).
🔥
A narrow band (20–40 mm) of the 3‑in pipe is heated to 1,650–2,050°F depending on material grade.
📐
The pipe is advanced at a controlled rate through the induction coil while the bending arm sweeps to the target radius of 36 in. The entire bend is formed in one continuous pass — no welds, no seams.
💧
The bend is water‑quenched and then tempered (or normalized) to restore the required mechanical properties and microstructure, verified by hardness and impact tests.
🔍
Each piece is checked for ovality ≤3% (min. required by ASME B16.49), wall thinning ≤12.5%, and angle tolerance ±0.5° using calibrated gauges and a digital protractor.
Quality gate: For every production lot, we batch‑test a sacrificial sample for tensile strength, yield strength, elongation, hardness (HV10), and Charpy V‑notch impact (at −20°F / −46°C as specified). Test reports are included in the shipment dossier. Need a third‑party inspection (SGS, Bureau Veritas, TÜV)? We coordinate — the cost is transparently quoted and typically $350–$650 per batch.
This product is not a general‑purpose commodity fitting. It earns its ROI in systems where flow efficiency, inspection access, and longevity outweigh initial cost. Typical installed environments include:
🛢️ Oil & Gas Gathering Lines
Used at launcher/receiver transitions and road crossings where smart‑pig traversal and code‑compliant ILI access are required. The 36‑in radius keeps hinge stresses below fatigue thresholds.
🏭 Chemical & Petrochemical Plants
For aggressive media where pressure drop impacts reactor feed pressure. Stainless and duplex versions resist chloride stress cracking.
💧 Water & Wastewater Treatment
Large‑radius bends prevent settling of solids at low flow rates, minimizing sludge accumulation inside direction changes.
⚡ Power Generation
Cooling water and boiler feedwater lines. The smooth interior reduces pressure pulsations and associated vibration in adjacent fittings.
🥤 Food & Beverage / CIP
Sanitary SS316L with Ra ≤ 0.8 μm finish enables complete clean‑in‑place drainage with no dead zones or accumulation pockets.
⛏️ Slurry & Mining
Hard‑wearing carbon steel with induction‑hardened intrados option extends service life by up to 2–3× compared to standard elbows in known abrasive service.
| Elbow Type | R/D | Pressure Drop (bar/elbow) | Relative Erosion |
|---|---|---|---|
| Short Radius (3 in R) | 1.0 | 0.049 | 100% (baseline) |
| Long Radius (4.5 in R) | 1.5 | 0.037 | 72% |
| 3R (9 in R) | 3.0 | 0.021 | 48% |
| 36 in Radius (this product) | 10.3 | 0.012 | 31% |
* Values calculated using Crane TP‑410 methods and erosion correlation from DNV‑RP‑O501. Individual results vary with media and operating conditions.
A Canadian oil sands producer replaced 54 standard 1.5D elbows on a produced‑water gathering line with our 3‑in 36‑in radius elbows during a 2024 remediation program.
Pigging speed increased by 22% — no more speed reductions through tight bends
Erosion‑related thickness readings improved — average wall loss at bends dropped from 0.32 mm/yr to 0.11 mm/yr
Operator extended inspection intervals from 12 to 20 months while maintaining integrity compliance
* Client approved publication of anonymized results.
TRUSTED BRANDS ACROSS ENERGY & INFRASTRUCTURE
Representative clients are shown above. NDA restrictions prevent displaying all logos.
It refers to a pipe elbow for a 3‑inch nominal bore (OD 3.5 in / 88.9 mm) pipe, with a 90° directional change, and a centerline bend radius of 36 inches (914.4 mm). The center‑to‑end distance on both openings is also 36 inches because for a 90° bend, the radius equals the center‑to‑end dimension. The R/D ratio of ~10.3 (OD based) makes this a very smooth long‑sweep fitting ideal for pigging and low‑pressure‑drop service.
The primary standard is ASME B16.49, which covers factory‑made, wrought‑steel induction bends for pipeline transportation and distribution systems. If the bend is also classified as a butt‑welding fitting in a piping system, ASME B16.9 dimensional requirements may apply. Design‑code compliance (ASME B31.3, B31.4, B31.8) must be confirmed by the project engineer; we supply full dimensional and material data to assist this verification.
Yes. Standard intelligent pigs are generally rated for bends with R/D ≥ 3. At R/D ≈ 10.3 (OD based), this elbow accommodates most MFL, UT, and calliper tools without speed reduction. We recommend confirming tool specifications with the pigging vendor, but margin is ample.
MOQ is 2 pieces for standard carbon steel grades. For stainless, MOQ may vary based on pipe availability. Current production lead time is 15–25 days after raw material confirmation. A small order of 2–10 pieces can often be produced within 15 days. Ocean freight to US Gulf Coast / Rotterdam / Felixstowe typically takes 25–40 days depending on the port.
The elbow is mounted on a steel‑reinforced wooden stillage with machined cradle blocks that contact only the straight tangent portions. It is then secured with ratchet straps and covered with stretch film plus an optional VCI (vapor‑corrosion inhibitor) paper. This prevents both movement damage and long‑term corrosion during transit. The total crate dimensions for a single piece are approximately 75 × 50 × 18 inches — we optimize multi‑piece stacking to minimize dimensional‑weight charges.
Yes. We can weld on ANSI/ASME B16.5 (Class 150–900) flanges before final heat treatment, or supply a flanged style for installation flexibility. Standard tangents are 12 in; custom tangent lengths are available. A flanged, 3‑in, 90°, 36‑in radius elbow is a common configuration in water treatment and temporary launcher applications.
Absolutely. We frequently work with SGS, Bureau Veritas, DNV, and TÜV. The inspection scope can include dimensional verification, hydrostatic testing, PMI (positive material identification), UT wall thickness, radiography on weld‑on attachments, and overseeing the hydro test witness. Third‑party costs are quoted separately, and we can coordinate the inspection date so that shipment isn't delayed.
For a 3‑in NPS, Sch 40 (0.216 in wall), A234 WPB, the allowable working pressure at room temperature is approximately 1,480 psi when calculated per ASME B31.3 (basic allowable stress 20,000 psi, weld joint factor 1.0). For Sch 80, the rating rises to approximately 2,120 psi. The bend itself does not reduce the pressure rating if produced per ASME B16.49 with wall thinning ≤12.5% — this is a key integrity advantage of the induction bending process. Always confirm final computations with the project design engineer.
Michael R.
Procurement Manager, US Midstream
“We ordered 120 pieces of the 3‑in 36‑in radius elbows for a Texas produced‑water line. Delivery took 21 days, and the dimensional report matched our internal verification within 0.02 inches. The seller actually saved us money by optimizing the crate layout — freight cost came in 18% under the initial estimate.”
Hassan A.
Project Director, Middle East EPC
“We used these elbows in a seawater injection system for a Gulf operator. The 316L stainless material was PMI‑verified by SGS on arrival. The smooth internal surface was visibly superior to a sample we requested from an Italian supplier. Will repeat.”
Ingrid S.
Operations Manager, German Chemical Plant
“We compared quotes from four Chinese suppliers. This team was the only one that answered technical questions about ovality tolerance and R6 integrity assessment without referring us to a junior clerk. The product documentation was audit‑ready.”
Get a comprehensive quotation within 24 business hours — including exact dimension data, material certificate samples, and a freight optimization proposal.
Written by Li Wei
Senior Pipeline Engineer & Export Director — Cangzhou Weihuan Pipeline Equipment Co., Ltd.
Li Wei has 16 years of experience in the manufacturing and international trade of pipe fittings, including 9 years specializing in induction bending and long‑radius pipeline elbows. He has personally overseen the delivery of more than 2,000 metric tons of fittings to 20+ countries and regularly contributes technical guidance for ASME B31 design reviews.

Aug 14,26
Industrial 3 inch threaded flange Standards and Applications
In the complex landscape of industrial piping, the selection of precision fittings is paramount to ensuring system longevity and operational safety. Among these critical components, the 3 inch threaded flange serves as a vital junction point, allowing for secure, leak-proof connections in medium-scale fluid transport systems across various manufacturing sectors. The global demand for high-performance structural metal products has surged as petrochemical and power energy plants evolve to handle higher pressures and more corrosive media. Utilizing a 3 inch threaded flange allows engineers to maintain structural integrity while ensuring that piping networks remain modular and easy to maintain

Jul 17,26
High Quality 6 inch threaded flange for Industrial Piping

May 06,26
High Quality Stainless Steel Threaded Pipe Flange Guide

Jun 23,26
High Performance 4 inch slip on flange and Socket Weld Flanges

Aug 10,26
High Quality 8 threaded flange for Industrial Piping Systems
In the complex world of structural metal fabrication, selecting the right piping components is critical for ensuring the integrity of high-pressure systems. The use of an 8 threaded flange, or more specifically, a socket weld alternative for small-bore piping, represents a strategic choice in balancing leak prevention with installation efficiency. Understanding the nuances of these connections is essential for engineers aiming to optimize safety and performance in demanding industrial environments. Global industrial standards, such as ASME B16.5, provide the necessary framework to ensure that components like the 8 threaded flange meet rigorous safety and pressure requirements.

Jun 18,26
Industrial Stainless Steel Slip On Flange Guide and Selection
SUBSCRIBE NEWSLETTER


