May. 22, 2026
In industrial piping systems, tees are essential fittings used to connect three sections of pipe and direct fluid flow. Among the many types available, seamless tees and welded tees are the two most widely used categories. Although they may appear similar externally, their manufacturing methods, structural integrity, pressure resistance, and application scenarios are significantly different.
Understanding the production process behind these two types of pipe fittings helps engineers, procurement managers, and industrial buyers choose the correct fitting for oil and gas, petrochemical, power generation, water treatment, and construction projects.
This article explains the complete difference between seamless tee and welded tee in the production process, including manufacturing methods, material performance, cost comparison, and industrial applications.
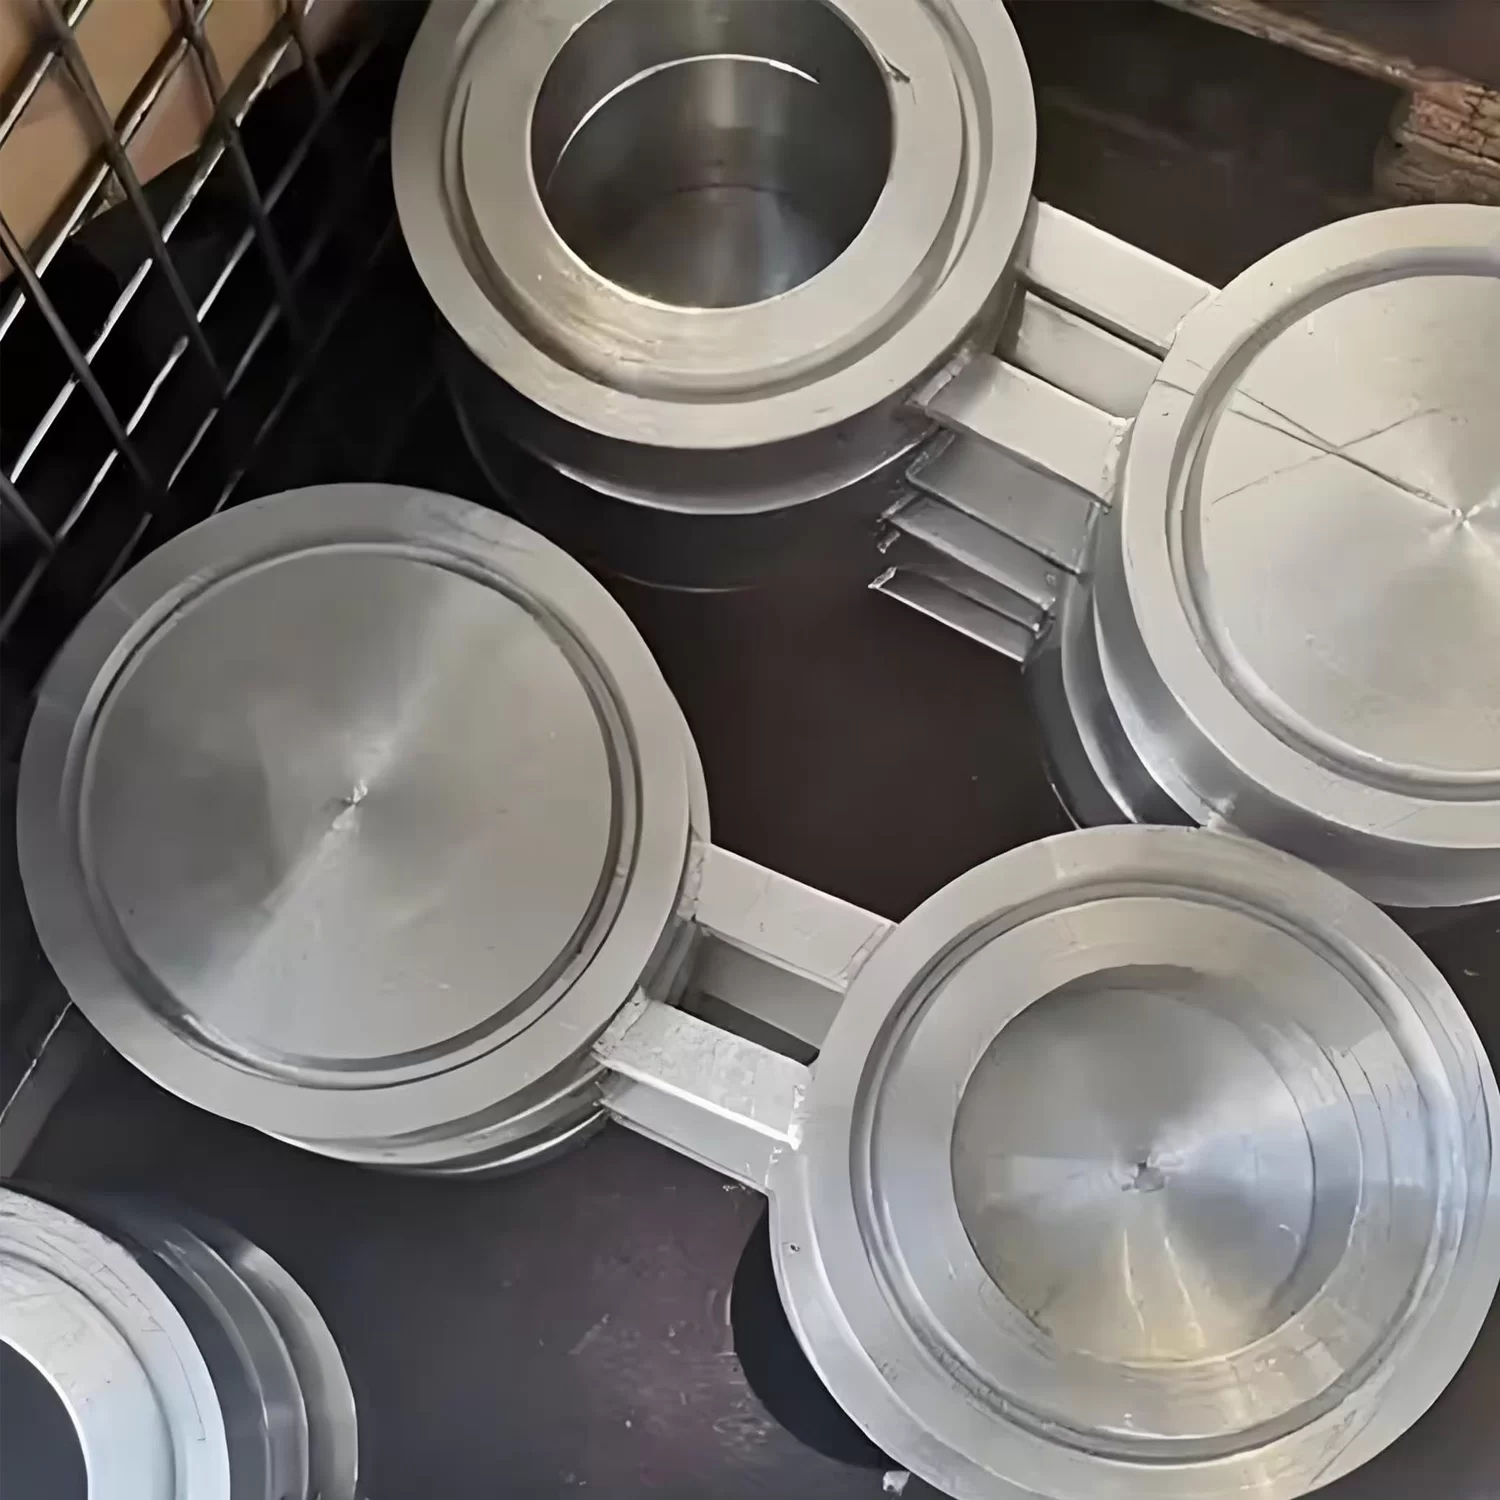
A seamless tee is a pipe fitting manufactured from a single piece of seamless steel pipe or forged billet without any welding seam. The branch outlet is formed through hot extrusion, hydraulic bulging, or forging processes.
Because there is no welded joint, seamless tees provide higher strength, better pressure resistance, and improved reliability under extreme working conditions.
Typical materials include:
Seamless tees are commonly manufactured according to standards such as:
A welded tee is produced by welding steel plates or steel pipes together to create the tee structure. Unlike seamless tees, welded tees contain one or more welding seams in the body or branch section.
This type of tee is widely used in low-pressure and large-diameter pipeline systems because it is more economical and easier to manufacture.

Welded tees can include:
The production method depends on pipe size, wall thickness, and application requirements.
The manufacturing process of seamless tees is more complex and requires advanced forming technology.
1. Raw Material Preparation
Manufacturers select high-quality seamless steel pipes or solid steel billets as raw materials. The material must meet strict chemical composition and mechanical property requirements.
After inspection, the billet is cut into the required length.
2. Heating Process
The steel material is heated in a furnace to a high forming temperature, usually between 1000°C and 1250°C depending on the material grade.
Uniform heating is critical because it affects:
Metal flow
Wall thickness consistency
Surface quality
Mechanical properties
3. Hot Extrusion or Hydraulic Bulging
This is the core production stage.
Hydraulic Bulging Method
In hydraulic bulging:
The pipe is placed inside a mold
High-pressure liquid is injected into the pipe
Internal pressure expands the branch outlet
External molds control the tee shape
This process ensures:
Smooth metal flow
Uniform wall thickness
Excellent structural integrity
Hot Extrusion Method
In hot extrusion:
A mechanical punch forces the heated material outward
The branch opening is formed directly from the parent pipe
No welding is involved
This method is often used for smaller-diameter tees.
4. Heat Treatment
After forming, the tee undergoes heat treatment such as:
Normalizing
Annealing
Quenching and tempering
Heat treatment improves:
Toughness
Strength
Stress distribution
Corrosion resistance
5. Machining and Surface Finishing
The tee is machined to achieve accurate dimensions and bevel angles.
Surface treatments may include:
Shot blasting
Pickling
Sandblasting
Anti-rust coating
6. Inspection and Testing
Seamless tees typically undergo strict testing procedures:
Ultrasonic testing
Radiographic testing
Hydrostatic pressure testing
Dimensional inspection
PMI testing
Because these fittings are often used in critical systems, quality control standards are extremely strict.
The welded tee manufacturing process is relatively simpler and more cost-effective.
1. Steel Plate or Pipe Selection
Manufacturers use steel plates or welded pipes as the raw material.
Material selection depends on:
Pipe diameter
Operating pressure
Corrosion environment
Temperature conditions
2. Cutting and Forming
The material is cut into sections using:
Plasma cutting
Laser cutting
Mechanical cutting
The branch section is shaped separately before assembly.
3. Welding Assembly
This is the defining stage of welded tee production.
The branch pipe is attached to the main pipe body using welding techniques such as:
TIG welding
MIG welding
Submerged arc welding
Manual arc welding
For large-diameter tees, multiple weld passes may be required.
4. Weld Seam Treatment
After welding, the seams are processed through:
Grinding
Polishing
Stress-relief heat treatment
Proper weld treatment reduces residual stress and improves mechanical performance.
5. Non-Destructive Testing
Welded tees also undergo inspection procedures including:
X-ray testing
Magnetic particle inspection
Dye penetrant testing
Ultrasonic testing
The weld seam is the primary focus during inspection.
1. Manufacturing Structure
2. Pressure Resistance
Seamless tees generally provide:
Welded tees may be suitable for:
3. Size Availability
Usually available in:
More suitable for:
4. Production Cost
Seamless tees are more expensive because:
Welded tees are more economical due to:
5. Production Efficiency
Welded tees can often be produced faster, especially for oversized dimensions.
Seamless tee production usually requires:
Industrial Applications
Seamless tees are commonly used in:
These industries require maximum reliability and leak prevention.
Welded tees are widely used in:
Their lower production cost makes them practical for general engineering projects.
When selecting a tee fitting, buyers should evaluate:
| Factor | Seamless Tee | Welded Tee |
|---|---|---|
| Pressure Resistance | Excellent | Moderate |
| Strength | Higher | Lower |
| Cost | Higher | Lower |
| Large Diameter Availability | Limited | Excellent |
| Corrosion Risk | Lower | Depends on weld quality |
| Manufacturing Complexity | High | Moderate |
If the system operates under extreme pressure, temperature, or corrosion conditions, seamless tees are usually the preferred option.
For large-scale projects with budget considerations and moderate operating conditions, welded tees may offer a more economical solution.
Conclusion
The main difference between seamless tee and welded tee lies in the production process. Seamless tees are manufactured from a single solid material through hot forming methods without welding, resulting in superior strength and reliability. Welded tees are fabricated by joining multiple steel sections through welding, making them more cost-effective and suitable for large-diameter applications.
Choosing the right tee depends on pipeline pressure, operating environment, project budget, and safety requirements. Understanding the manufacturing process helps industrial buyers make informed procurement decisions and improve long-term pipeline performance.
For critical industrial systems where durability and safety are priorities, seamless tees remain the premium choice. For general engineering and large pipeline projects, welded tees provide flexibility and cost efficiency.

Aug 14,26
Industrial 3 inch threaded flange Standards and Applications
In the complex landscape of industrial piping, the selection of precision fittings is paramount to ensuring system longevity and operational safety. Among these critical components, the 3 inch threaded flange serves as a vital junction point, allowing for secure, leak-proof connections in medium-scale fluid transport systems across various manufacturing sectors. The global demand for high-performance structural metal products has surged as petrochemical and power energy plants evolve to handle higher pressures and more corrosive media. Utilizing a 3 inch threaded flange allows engineers to maintain structural integrity while ensuring that piping networks remain modular and easy to maintain

Aug 17,26
High Quality stainless steel threaded pipe flange and Weld Neck Flanges
The selection of high-performance piping components is critical for the structural integrity of any industrial fluid transport system. Among these, the use of specialized flanges ensures that connections can withstand intense operational stresses without compromising safety. Understanding the technical nuances of these components is essential for engineers aiming to minimize downtime and prevent catastrophic leaks in high-pressure environments. In the global manufacturing landscape, the demand for precision-engineered connectors has surged as industries push the boundaries of temperature and pressure. From petrochemical plants to nuclear facilities, the ability to create a seamless, leak-proof seal is not just a technical requirement but a safety imperative.

Aug 10,26
High Quality 8 threaded flange for Industrial Piping Systems
In the complex world of structural metal fabrication, selecting the right piping components is critical for ensuring the integrity of high-pressure systems. The use of an 8 threaded flange, or more specifically, a socket weld alternative for small-bore piping, represents a strategic choice in balancing leak prevention with installation efficiency. Understanding the nuances of these connections is essential for engineers aiming to optimize safety and performance in demanding industrial environments. Global industrial standards, such as ASME B16.5, provide the necessary framework to ensure that components like the 8 threaded flange meet rigorous safety and pressure requirements.
Apr 07,26
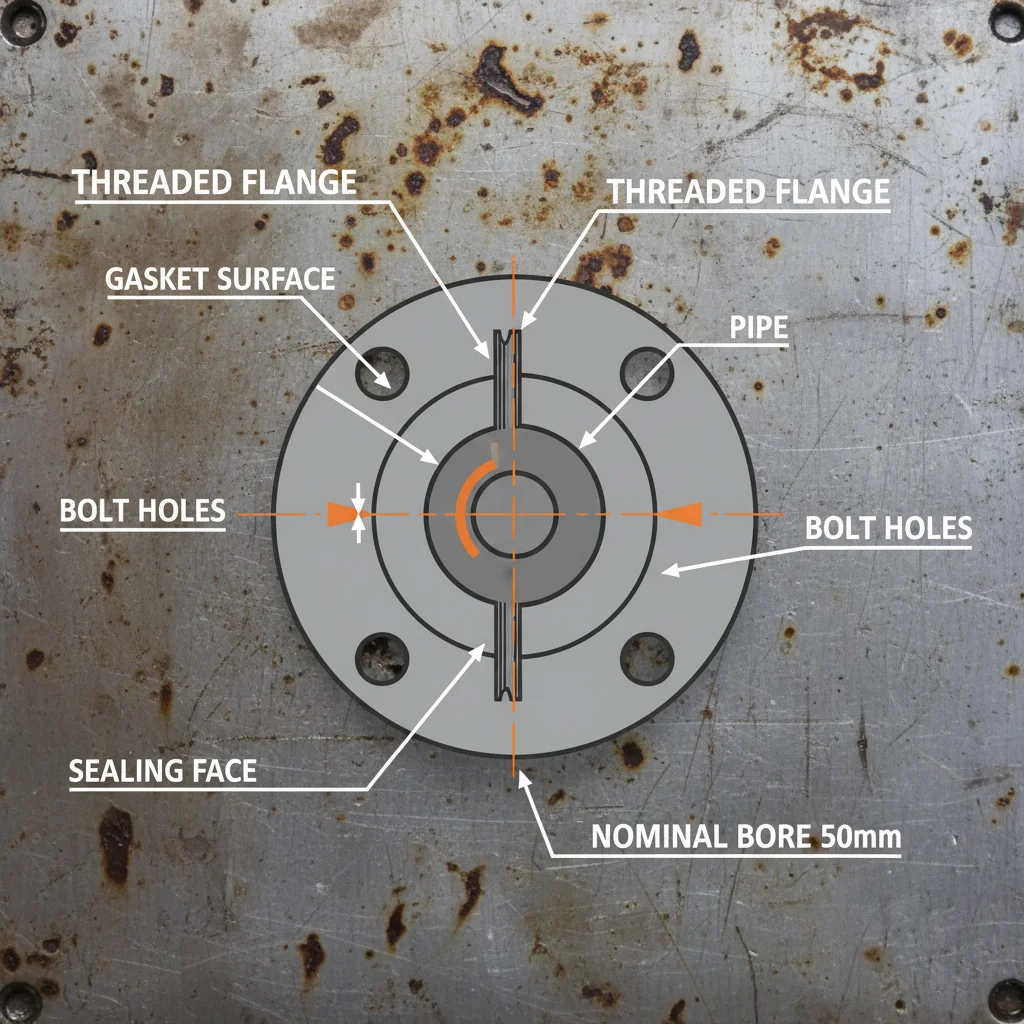
Understanding 50mm Threaded Flange Specifications for Global Commerce

Aug 21,26
Industrial Grade 1 1 4 Threaded Flange for Piping Systems
The selection of precision piping components is critical for maintaining the structural integrity and flow efficiency of industrial fluid systems. Among these, the 1 1 4 threaded flange serves as a fundamental connection point, ensuring leak-proof transitions in a variety of pressurized environments. Understanding the nuances of its design and application is essential for engineers aiming to minimize downtime and maximize operational safety. In the global manufacturing landscape, the demand for standardized yet high-performance fittings has led to the widespread adoption of specific threaded configurations. The 1 1 4 threaded flange addresses the need for a secure, mechanical joint

May 25,26
Common Materials Used in 90° Elbow Production and Their Advantages
In modern pipeline systems, the 90° elbow plays a critical role in changing flow direction while maintaining pressure integrity and operational efficiency. Whether used in oil and gas pipelines, chemical plants, water treatment facilities, or HVAC systems, selecting the right material for a 90-degree elbow directly affects durability, corrosion resistance, temperature tolerance, and overall service life.
SUBSCRIBE NEWSLETTER